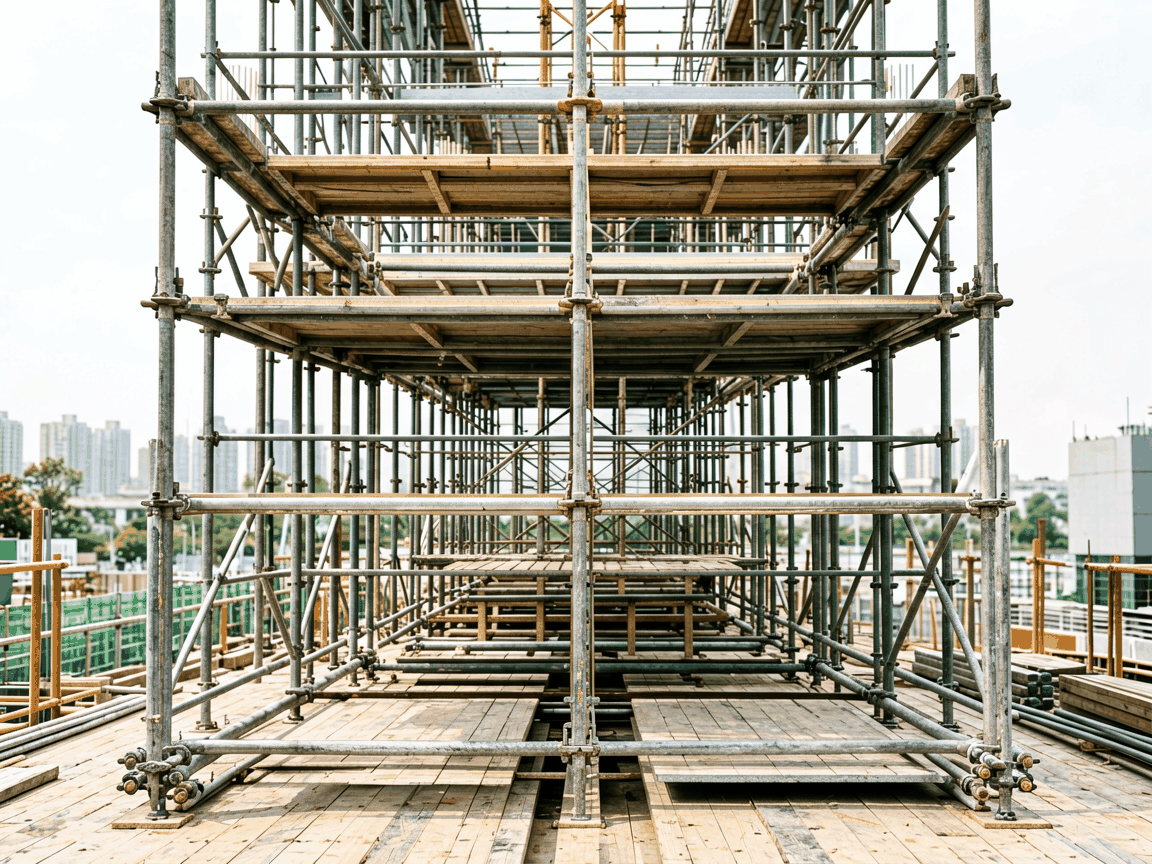
A parallel coupler is a critical connection component in tube-and-coupler scaffolding systems, designed to join two scaffold tubes at a precise 90-degree angle while maintaining parallel alignment of their longitudinal axes. Unlike swivel or adjustable couplers, it provides a rigid, fixed-right-angle joint essential for creating stable horizontal and vertical frames, ledgers, and transoms in modular scaffolding structures. Its primary function is to transfer both axial and shear loads between connected tubes without relative movement, ensuring structural integrity under dynamic site conditions.
Manufactured from high-strength steel grades such as S355JR or equivalent, the coupler body undergoes hot forging or precision casting to achieve uniform grain structure and eliminate internal defects. The internal jaws are machined to tight tolerances (typically ±0.5mm) to ensure full circumferential contact with scaffold tubes of standard nominal diameters (48.3mm OD). This precision fit minimizes stress concentrations and prevents tube slippage under load, which is vital for maintaining safety factors in temporary works design.
The coupler incorporates two parallel bolts—usually M16 or M20 grade 8.8 high-tensile steel—each equipped with a captive washer and nut to prevent loss during assembly. Tightening torque is specified between 80–100 Nm for M16 bolts, generating sufficient clamping force to overcome the coefficient of friction between steel surfaces (typically 0.15–0.25 for dry, unlubricated interfaces) and resist loosening due to vibration. This bolted mechanism allows for rapid, repeatable assembly and disassembly without damaging the tube or coupler threads.
The load capacity of a parallel coupler is not defined by a single value but depends on the interaction between tube strength, coupler geometry, bolt preload, and connection configuration. In typical ledger-to-transom junctions, the coupler resists shear forces parallel to the tube axis and tension/compression forces perpendicular to it. Design calculations per EN 12810-1 or equivalent standards consider the coupler as a rigid joint with moment resistance derived from the bolt couple and tube wall thickness.
For a standard 48.3mm x 3.2mm tube connected via a forged S355JR coupler with two M16 8.8 bolts tightened to 90 Nm, the characteristic shear resistance typically exceeds 20 kN per shear plane, while tensile capacity perpendicular to the tube axis can reach 15–18 kN depending on effective bearing area. These values are verified through routine type testing and are subject to reduction factors for long-term use, corrosion, or repeated cycling as specified in local scaffolding regulations.
Corrosion protection is achieved through hot-dip galvanizing to a minimum coating thickness of 55 microns (average 70 microns) per EN ISO 1461, providing durable barrier protection in outdoor construction environments. The galvanized layer sacrifices itself to protect the underlying steel, extending service life to 5–10 years in typical atmospheric conditions without maintenance. Alternative coatings such as sherardizing or mechanical plating may be specified for applications requiring consistent thread engagement or reduced coating thickness.
The internal geometry of the coupler jaws is critical to performance. Rather than relying on sharp edges or point loading, the bearing surfaces are contoured to distribute pressure evenly across approximately 60–70% of the tube circumference. This design reduces localized deformation and prevents ovalization of the tube under repeated load cycles. Jaw depth is typically 25–30mm to ensure sufficient overlap with the tube, resisting peeling forces that could cause gradual disengagement.
Bolt holes are drilled and reamed after forging or casting to achieve perpendicular alignment with the coupler body, ensuring that bolt tension translates directly into clamping force without inducing bending stresses. The distance between bolt centers is standardized (usually 60–70mm) to match common tube spacing in scaffolding bays, enabling compatibility with ledgers and transoms of varying lengths. This dimensional consistency allows interchangeability between couplers from different manufacturers that adhere to the same tube standard.
Manufacturing quality control includes dimensional inspection of jaw geometry, bolt hole perpendicularity, and thread integrity. Each batch undergoes proof load testing on a sample basis, where couplers are assembled with tubes and subjected to incremental loads until deformation or slip occurs. Traceability is maintained via batch codes stamped on the coupler body, linking each unit to its material certificate, heat treatment record, and inspection documentation.
Parallel couplers are fundamental to constructing facade scaffolding where vertical standards are connected to horizontal ledgers at each lift level. In this configuration, the coupler ensures that the ledger remains perfectly horizontal, which is essential for maintaining uniform platform height and preventing tripping hazards. The rigidity of the joint also resists racking forces caused by wind loads or uneven settlement, preserving the squareness of the scaffold bay.
In birdcage scaffolds used for interior work such as ceiling installation or soffit repairs, parallel couplers join ledgers and transoms to form a grid-like horizontal plane at each level. The fixed 90-degree angle guarantees orthogonal alignment, which is critical for evenly distributing loads across multiple standards and preventing localized overstress. This application benefits from the coupler’s ability to withstand reversed cyclic loads during repeated assembly and disassembly cycles.
For cantilever scaffolds or loading bays, parallel couplers secure tie tubes to the main structure at right angles, transferring lateral forces from the scaffold back to the building or ground anchors. The coupler’s resistance to rotation under load ensures that tie tubes remain perpendicular to the facade, maximizing their effectiveness in resisting outward movement. Proper selection and installation of these couplers are often scrutinized during temporary works approval due to their role in overall system stability.
While standard parallel couplers are designed for 48.3mm nominal diameter tubes, variants exist for other common scaffold tube sizes such as 42.4mm or 60.3mm OD, particularly in specialized systems or regional markets. The coupler’s internal bore is precision-machined to match the specific tube diameter, with wall thickness accommodation typically ranging from 2.5mm to 4.0mm to suit different tube schedules. Custom lengths or jaw profiles are uncommon due to the functional constraints of the 90-degree joint, but bolt size and grade can be adjusted based on project-specific load requirements.
Material selection extends beyond carbon steel to include low-alloy variants for enhanced strength-to-weight ratios or stainless steel grades (e.g., 304 or 316) for corrosive environments such as chemical plants, coastal areas, or food processing facilities. In stainless steel versions, galling prevention is addressed through surface treatments or the use of dissimilar materials for bolts and nuts, ensuring reliable disassembly after extended exposure. Hot-dip galvanizing remains incompatible with stainless steel, so alternative protections like passivation or clear sealers are used.
Thread protection is a key consideration in reusable couplers. Bolts are often supplied with nylon inserts or patch lock elements to resist vibrational loosening without requiring frequent retightening. Some designs incorporate captive bolt assemblies where the bolt cannot be fully removed from the coupler body, reducing the risk of lost parts on busy construction sites. These features improve operational efficiency and reduce downtime during scaffold erection and dismantling.
Quality assurance begins with material verification, where incoming steel is checked for chemical composition and mechanical properties against mill test certificates. For forged couplers, grain flow orientation is visually or magneto-inductively inspected to ensure it follows the high-stress paths around the jaw and bolt holes. Non-destructive testing such as magnetic particle inspection may be applied to critical areas to detect surface or subsurface cracks that could propagate under cyclic loading.
Functional testing includes torque-tension analysis to validate the relationship between applied bolt torque and resulting clamping force, accounting for friction variables. Slide-off resistance tests simulate the peeling force that attempts to disengage the tube from the coupler jaws, with acceptance criteria typically set above 1.5 times the expected service load. Repeatability is assessed by subjecting couplers to multiple assembly-disassembly cycles to ensure no degradation in jaw geometry or thread condition.
Final inspection includes visual checks for coating uniformity, thread cleanliness, and absence of casting flashes or forging laps. Dimensions are verified using gauges or coordinate measuring machines (CMM) on a statistical sample basis. Each coupler is marked with size, material grade, batch number, and manufacturer identifier, enabling full traceability throughout its lifecycle. These records support compliance with standards such as EN 74, ANSI/SSFI SC100.5-04, or AS/NZS 1576.2.
| Parameter | Typical Value / Range | Notes |
|---|---|---|
| Tube Compatibility | 48.3mm OD (standard) | Also available for 42.4mm, 60.3mm upon request |
| Material Grade | S355JR (carbon steel) | Stainless steel 304/316 available for corrosive environments |
| Bolt Size | M16 or M20 | Grade 8.8 high-tensile steel |
| Recommended Torque | 80–100 Nm (M16) | Generates sufficient preload to resist vibration loosening |
| Coating | Hot-dip galvanized | Min. 55 microns; alternative coatings available |
| Shear Resistance (per plane) | >20 kN | Dependent on tube & bolt specs; verified via testing |
| Service Life | 5–10 years | In typical atmospheric conditions with galvanizing |
Procurement specifications should reference the coupler’s compatibility with the intended scaffold tube diameter and wall thickness, as mismatched components can lead to unsafe connections. Buyers are advised to request material test certificates (MTCs) and test reports verifying mechanical properties and coating thickness. For projects with unique requirements—such as offshore, high-corrosion, or architectural scaffolding—customization of material grade, bolt type, or coating system is typically available following technical review.
Lead times for standard parallel couplers generally range from 2–4 weeks for stock items and 6–8 weeks for customized orders, depending on material availability and production scheduling. Samples can be provided for evaluation upon request, allowing engineering teams to verify fit, finish, and compatibility with existing inventory. Packaging is typically in bulk cartons or palletized units with corrosion-inhibiting separators to prevent damage during transit and storage.
Technical support includes assistance with load calculations, joint detailing, and compliance with local scaffolding regulations. Manufacturers often provide CAD models or BIM objects to facilitate integration into temporary works design software. This level of support reduces the risk of specification errors and ensures that the coupler performs as intended throughout the scaffold’s lifecycle, from erection to dismantling.





