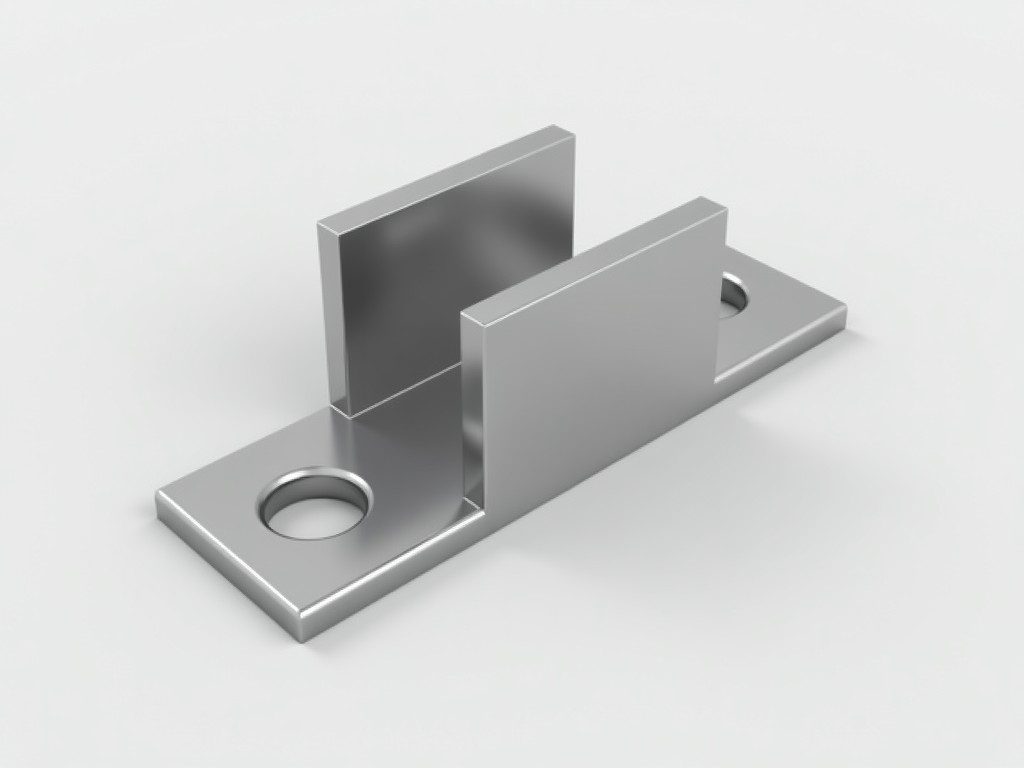
Panel clamps designated as 2-3-8 refer to a standardized mounting system where the numerals indicate hole spacing in millimeters: 2mm, 3mm, and 8mm intervals between fastening points. This configuration is commonly used in modular enclosure systems, control panel fabrication, and equipment racking where precise alignment and repeatable fastening are critical. Understanding the dimensional logic behind this designation enables engineers to select compatible components without relying on proprietary branding.
The 2-3-8 panel clamp derives its name from the sequential hole pattern: two holes spaced 2mm apart, followed by a 3mm gap to the next pair, then an 8mm interval to the final set. This staggered arrangement prevents rotational misalignment during installation while allowing limited lateral adjustment within the mounting plane. The clamp body typically features a C-channel or U-shaped profile with pre-drilled or threaded holes matching this pattern, enabling secure attachment to panels ranging from 1.2mm to 3.0mm thickness using machine screws or self-tapping fasteners.
Unlike symmetrical hole patterns, the asymmetric 2-3-8 layout introduces a mechanical keying effect. When installed, the clamp resists both axial pull-off and tangential shear forces due to the uneven distribution of load paths. This makes it particularly effective in vibration-prone environments such as motor control centers, transportation electronics, and industrial automation enclosures where sustained mechanical stability is required.
Common materials for 2-3-8 panel clamps include cold-rolled steel with zinc plating, stainless steel (grades 304 and 316), and aluminum alloys (6061-T6). Zinc-plated steel offers adequate corrosion resistance for indoor, dry environments with a typical salt spray endurance of 96 hours per ASTM B117. Stainless steel variants extend this to 500+ hours and are preferred in food processing, pharmaceutical, or outdoor telecom enclosures where exposure to moisture, cleaning agents, or salt spray is expected.
Aluminum clamps provide a strength-to-weight ratio advantageous in portable equipment or aerospace-adjacent applications, though they require careful consideration of galvanic corrosion when coupled with dissimilar metals. Surface treatments such as clear anodizing or chromate conversion coating can mitigate this risk. Material thickness typically ranges from 1.5mm to 2.5mm, balancing stiffness with ease of forming during manufacturing.
The maximum static load capacity of a standard 2-3-8 panel clamp depends on material, fastener size, and panel thickness. For a 2.0mm thick zinc-plated steel clamp using M3 machine screws, the typical tensile strength is approximately 180N per clamp, with shear resistance rated at 220N. These values assume proper torque application (0.5–0.7 Nm for M3) and full thread engagement. Exceeding these limits may cause panel deformation or fastener pull-through, particularly in softer materials like ABS or polycarbonate enclosures.
Installation requires alignment of the clamp’s hole pattern with matching receptacles on the panel or chassis. A pilot hole diameter of 2.5mm is recommended for M3 screws in metal panels to prevent cracking, while self-tapping variants may use a 2.2mm starter hole. Torque should be applied incrementally in a cross-pattern if multiple clamps are used per panel to avoid warping. Always verify panel flatness within 0.1mm tolerance over the clamping zone to ensure even load distribution.
The 2-3-8 panel clamp is frequently employed in the assembly of DIN rail-mounted terminal blocks, where the spacing aligns with standard terminal block pitch dimensions. This allows technicians to secure grounding lugs, surge protectors, or signal isolators directly to the enclosure backplane without additional brackets. In machine tool control panels, these clamps facilitate rapid replacement of I/O modules by maintaining precise positional tolerances during rework.
In telecommunications infrastructure, the pattern supports the mounting of fiber optic splice trays and copper distribution frames within NEMA-rated cabinets. The asymmetric hole layout ensures that once installed, the clamp cannot be rotated 180 degrees and reinstalled incorrectly — a critical feature for maintaining signal integrity and grounding continuity. Similarly, in automotive electronics housings, the design prevents misalignment of sensor harnesses during vibration testing.
Compared to symmetrical hole patterns (e.g., 3-3-3 or 4-4-4), the 2-3-8 configuration offers superior resistance to rotational settling under cyclic loading. Symmetrical designs may allow micro-movement over time as vibrations align with the hole axis, gradually loosening fasteners. The staggered 2-3-8 pattern disrupts this resonance by creating uneven load paths that dissipate energy more effectively.
Unlike adhesive-based or snap-fit alternatives, mechanical clamps provide predictable, quantifiable holding force that does not degrade with temperature cycling or UV exposure. While quick-release levers offer convenience, they typically sacrifice load capacity and are unsuitable for permanent installations requiring IP ratings. The 2-3-8 clamp strikes a balance between installability, mechanical integrity, and long-term reliability in fixed industrial assemblies.
Dimensional accuracy of the hole pattern is critical to function. Tolerances on hole spacing are typically held to ±0.1mm using CNC punching or stamping dies with hardened tooling. Hole diameter consistency ensures proper screw engagement and prevents cross-threading. Post-forming operations such as deburring and edge rolling are performed to eliminate sharp edges that could damage panel coatings or injure assemblers.
Material certification is verified at intake, with mill test reports confirming composition and mechanical properties. Finished clamps undergo visual inspection for coating uniformity, bending accuracy, and absence of cracks or splits. Functional validation may include torque-to-failure testing on a sample batch to confirm load ratings. Traceability is maintained via lot numbers linked to material heat numbers and production shifts.
While the 2-3-8 hole pattern is standardized, several parameters can be adapted to suit specific project requirements. Clamp length can be extended to accommodate wider panels or to provide additional mounting points for cable ties or conduit brackets. Material thickness may be increased to 3.0mm for high-vibration applications or reduced to 1.2mm for lightweight enclosures where minimal protrusion is essential.
Alternative finishes include black zinc nickel for enhanced corrosion resistance in harsh environments, or powder coating in RAL colors to match enclosure aesthetics. Custom hole patterns derived from the 2-3-8 base — such as adding a fifth hole for grounding lugs — are feasible upon engineering review. All modifications are subject to revalidation of load capacity and dimensional compliance.
For technical inquiries, customization requests, or sample evaluation, contact our engineering team to discuss your specific panel clamping needs.





